

Water is a key material in pharmaceutical manufacturing. It is used as an ingredient, for cleaning, and as a raw material. For sterile and injectable products, Water for Injection (WFI) must meet much tighter rules than normal process water. This is why pharmaceutical companies need a reliable water generation system.
Multi-Effect Distillation is a well-known technology for producing WFI. It uses several evaporation stages to reuse heat from secondary steam. This design can lower steam use compared with a single-effect distiller. At the same time, it keeps a high level of separation between water and non-volatile impurities.
This guide explains the multi effect distillation working principle, the multi effect distillation process, its benefits, and key points when selecting pharmaceutical water distillation equipment.
What Is Multi-Effect Distillation (MED)?
Multi-Effect Distillation, often called MED, is a thermal process. It uses several evaporator stages, known as effects. Each effect runs at a lower pressure and temperature than the one before it.
The main idea is heat reuse. In the first effect, outside plant steam provides the main heating energy. When the feed water boils, it makes secondary steam. Instead of sending this steam to waste, the system uses it as the heating source for the next effect.
The second effect runs at a lower pressure. Because of this, the secondary steam from the first effect can condense and give its heat to the feed water in the second effect. The same thing happens again and again in the later effects.
This process lets the system reuse thermal energy many times. Adding more effects can improve steam economy. But it also raises equipment cost and system complexity. So the best number of effects depends on the plant’s steam supply, required capacity, and budget.
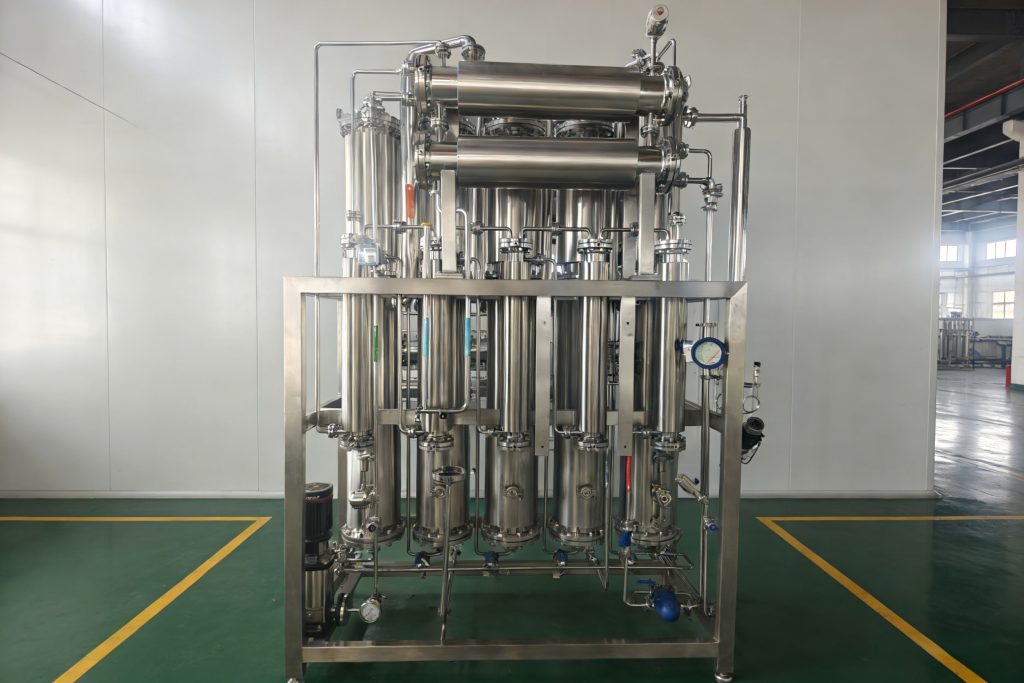
Modern pharmaceutical multi effect distillation MED systems often use falling-film evaporation. In this design, feed water forms a thin film on the heating surface and flows down through the evaporator tubes. This supports efficient evaporation and stable operation.
Multi-Effect Distillation Working Principle
The multi effect distillation working principle is based on a simple idea. Steam carries heat. When steam condenses, it releases that heat. A MED system uses this idea again and again across several effects.
In the first effect, plant steam heats the feed water. Part of the water boils and becomes secondary steam. This secondary steam still holds a lot of thermal energy. Instead of being wasted, it becomes the heating source for the second effect.
The second effect runs at a lower pressure than the first. This lower pressure lets the secondary steam condense at a lower temperature. As it condenses, it gives off heat and boils more feed water. The vapor made there then moves to the third effect.
This cycle repeats through all effects. Only the first effect needs outside plant steam. Each later effect is driven by the vapor from the effect before it. The final vapor is condensed in a final condenser.
So the multi effect distillation working principle gives two key results. First, it separates water from non-volatile impurities through evaporation. Second, it reuses heat many times. This lowers steam use per liter of WFI produced.
Multi-Effect Distillation Process Step by Step
The multi effect distillation process has several connected stages. Each stage must be controlled to protect WFI quality.
1. Feed Water and Preheating
The feed water for a pharmaceutical multi effect distillation MED system is normally Purified Water. It must meet the applicable pharmacopoeia requirements. Before entering the first effect, the feed water passes through a preheater. Heat recovered from the distillation process raises the feed temperature. This lowers the heating duty needed from the primary steam source.
Feed-water quality is important. A stable PW supply helps reduce scaling, corrosion, and contamination risks. It also supports consistent MED performance.
2. Evaporation in the First Effect
In the first effect, plant steam gives heat to the feed water. Part of the water boils and becomes secondary steam. The liquid phase becomes more concentrated. This is because many non-volatile substances stay in the liquid instead of entering the vapor phase. The vapor then passes through a separation system before moving to the next effect.
Good vapor-liquid separation is essential. If liquid droplets are carried with the steam, they may contain impurities. Good separator design therefore helps protect the quality of the vapor.
3. Heat Recovery Through Later Effects
The secondary steam from the first effect becomes the heating medium for the second effect. The second effect runs at a lower pressure. So the secondary steam can condense while giving heat to the next feed-water stream. The same process repeats in the third, fourth, and later effects.
This is the key benefit of the multi effect distillation process. Instead of using fresh plant steam for every stage, the system reuses thermal energy from the effect before it. Actual steam use depends on the full system design and operating conditions.
4. Final Condensation and WFI Collection
After the final evaporation effect, the remaining vapor goes to the final condenser. Depending on the system design, feed water, cooling water, or another utility may be used for condensation. The product water is collected through sanitary piping and sent to the WFI storage and distribution system.
Online instruments can monitor key process parameters. These include conductivity, temperature, pressure, and flow. Other WFI quality attributes, such as TOC, microbial quality, and endotoxin, are controlled through a validated sampling and testing program.
Why MED Is Used for WFI
WFI has strict quality requirements. It may be used in the manufacture of parenteral products and other applications with high microbiological control needs.
Distillation provides an important physical separation step. During evaporation, water changes from liquid to vapor. Many non-volatile substances stay in the liquid phase. Proper vapor separation further reduces the risk of droplets entering the product stream.
Endotoxin Control
Bacterial endotoxins are linked to the cell walls of Gram-negative bacteria. They are not reliably controlled by normal filtration alone. They need specific control strategies.
A well-designed multi effect distillation MED system can provide strong endotoxin reduction. This comes from evaporation and effective vapor-liquid separation. In practice, a good system can achieve several log reductions of endotoxin. However, MED should not be the only endotoxin-control measure.
Feed-water quality, equipment hygiene, storage, distribution, sanitization, and operating procedures are also important.
Efficient Heat Reuse
The major engineering benefit of MED is the reuse of secondary steam. The first effect receives outside heating energy. The vapor made by this effect is then reused in the next effect. This lowers the amount of fresh steam needed. It is much better than systems where each stage needs its own heat source.
More effects can improve steam economy. But the benefit must be balanced against higher capital cost and greater system complexity.

Multi-Effect Distillation vs. Vapor Compression
Multi-Effect Distillation is not the only thermal technology for pharmaceutical water production. Vapor compression (VC) distillation uses a different energy strategy. It compresses generated vapor to raise its temperature and pressure. Then the vapor can be reused as a heating source.
| Feature | Multi-Effect Distillation (MED) | Vapor Compression Distillation |
|---|---|---|
| Main energy source | Plant steam | Electrical energy for vapor compression |
| Heat reuse | Secondary steam is reused between effects | Compressed vapor is reused |
| Plant steam requirement | Required for the heating side | Can be lower depending on design |
| Electricity demand | Mainly for pumps and controls | Higher because of the compressor |
| Main selection factor | Steam availability and production capacity | Electrical capacity and operating strategy |
| System design | Multiple evaporation effects | Compressor-based thermal cycle |
Neither technology is right for every pharmaceutical plant. The choice should consider WFI demand, available utilities, energy cost, installation conditions, maintenance, and the overall water-system design.
Key Technical Features of a Pharmaceutical MED System
A pharmaceutical multi effect distillation MED system should be designed around more than heat-transfer efficiency. Hygienic construction, cleanability, separation performance, instruments, and validation support are equally important.
| Aspect | Typical MED Design Consideration |
|---|---|
| Feed water | Purified Water suitable for the intended WFI process |
| Evaporator | Falling-film or other validated sanitary evaporation design |
| Number of effects | Selected by capacity, steam supply, and energy targets |
| Main material | SS316L for wetted product-contact parts |
| Surface finish | Defined by project and sanitary design requirements |
| Vapor separation | Gravity, demister, centrifugal, or combined separation |
| Heat recovery | Secondary steam and feed-water preheating |
| Monitoring | Pressure, temperature, flow, conductivity and other key parameters |
| Engineering standards | Applicable GMP, pharmacopoeia, and project requirements |
The exact specifications should always be checked against the equipment design, project URS, and applicable regulations.
SKE&EAGLE Multi-Effect Distillation Solutions
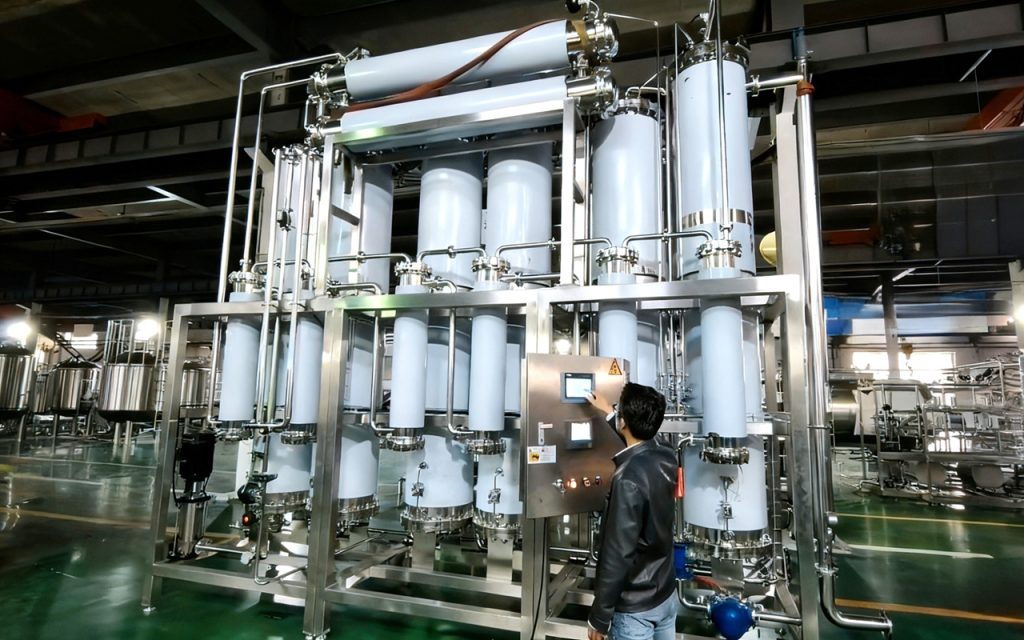
SKE&EAGLE provides pharmaceutical water equipment for commercial pharmaceutical production. Its multi effect distillation MED systems are designed for WFI applications. They can be configured by project capacity and utility conditions.
The equipment can use sanitary SS316L construction for product-contact components. It can also include hygienic surface treatment and sanitary piping. The system design can integrate heat recovery, multi-stage vapor separation, automatic control, online monitoring, and connection with WFI storage and distribution systems.
SKE&EAGLE’s MED design uses multiple protection stages to support vapor purity. Falling-film evaporation provides efficient heat transfer. Downstream steam-water separation helps reduce the carryover of liquid droplets.
For pharmaceutical manufacturers, equipment selection should be based on the full system, not only the distiller itself. SKE&EAGLE can evaluate WFI capacity, steam conditions, feed-water quality, storage requirements, distribution design, automation, and project validation needs.
Frequently Asked Questions
1. What is multi effect distillation used for?
Multi-Effect Distillation is mainly used as a thermal technology for producing high-purity pharmaceutical water, including WFI.
2. What does MED stand for in pharmaceutical water systems?
MED stands for Multi-Effect Distillation. It is a thermal process that uses several evaporation effects to reuse heat and produce purified water such as WFI.
3. What is the multi effect distillation working principle?
The multi effect distillation working principle is heat reuse. The first effect uses plant steam. The vapor from each effect becomes the heating source for the next effect. Because each effect runs at lower pressure, the secondary steam can condense and release heat.
4. How many effects are used in a pharmaceutical MED system?
The number of effects depends on production capacity, available plant steam, energy targets, and budget. There is no single number that is right for every system.
5. Can MED remove bacterial endotoxins?
Distillation and effective vapor-liquid separation can provide strong endotoxin reduction. In practice, it can reach several log reductions. However, endotoxin control also depends on feed-water quality, equipment hygiene, storage, and validated operating procedures.
6. Is MED better than vapor compression distillation?
The two technologies use different energy strategies. MED relies mainly on plant steam and heat reuse. Vapor compression uses electrical energy to compress vapor. The right choice depends on the plant’s utilities, capacity, and project requirements.
Conclusion
Multi-Effect Distillation is a well-established thermal technology for pharmaceutical WFI production. Its main benefit is the reuse of secondary steam across several evaporation effects. This can improve steam economy while supporting a controlled distillation process.
However, a high-quality pharmaceutical multi effect distillation MED system is more than a series of evaporators. Feed-water quality, vapor-liquid separation, sanitary construction, instruments, heat recovery, storage, distribution, and validation all affect the final system performance.
With experience in pharmaceutical water equipment, SKE&EAGLE provides multi effect distillation solutions. They can be configured for different WFI production requirements, utility conditions, and project validation needs.
Official Website: https://www.ske-eagle.com/
Contact Email: info@ske-eagle.com
Follow us on Facebook for the latest industry insights: SKE & Eagle Facebook
Business Inquiries: Visit our official website and submit the contact form at the bottom.