
Water is one of the most important raw materials in pharmaceutical manufacturing. It is used in drug formulation, equipment cleaning, laboratory testing, and many production processes. However, pharmaceutical water is not ordinary process water. It must meet strict quality requirements for chemical purity, microbial control, and endotoxin levels.
A reliable pharmaceutical water preparation system is the foundation for producing consistent and compliant pharmaceutical water. Depending on product requirements, pharmaceutical companies may need different water grades, including Purified Water (PW) and Water for Injection (WFI).
This guide explains pharmaceutical water grades, purification technologies, WFI production methods, system selection factors, and validation requirements to help manufacturers understand how to build an efficient and GMP-compliant water system.
Pharmaceutical Water Grades and Applications
Pharmaceutical water is classified into different grades according to its quality requirements and intended use. The selection of water grade depends mainly on the final product type, manufacturing process, and regulatory requirements.
Purified Water (PW)
Purified Water is the most commonly used pharmaceutical process water. It is widely applied in non-sterile pharmaceutical production, equipment cleaning, laboratory applications, and preparation processes.
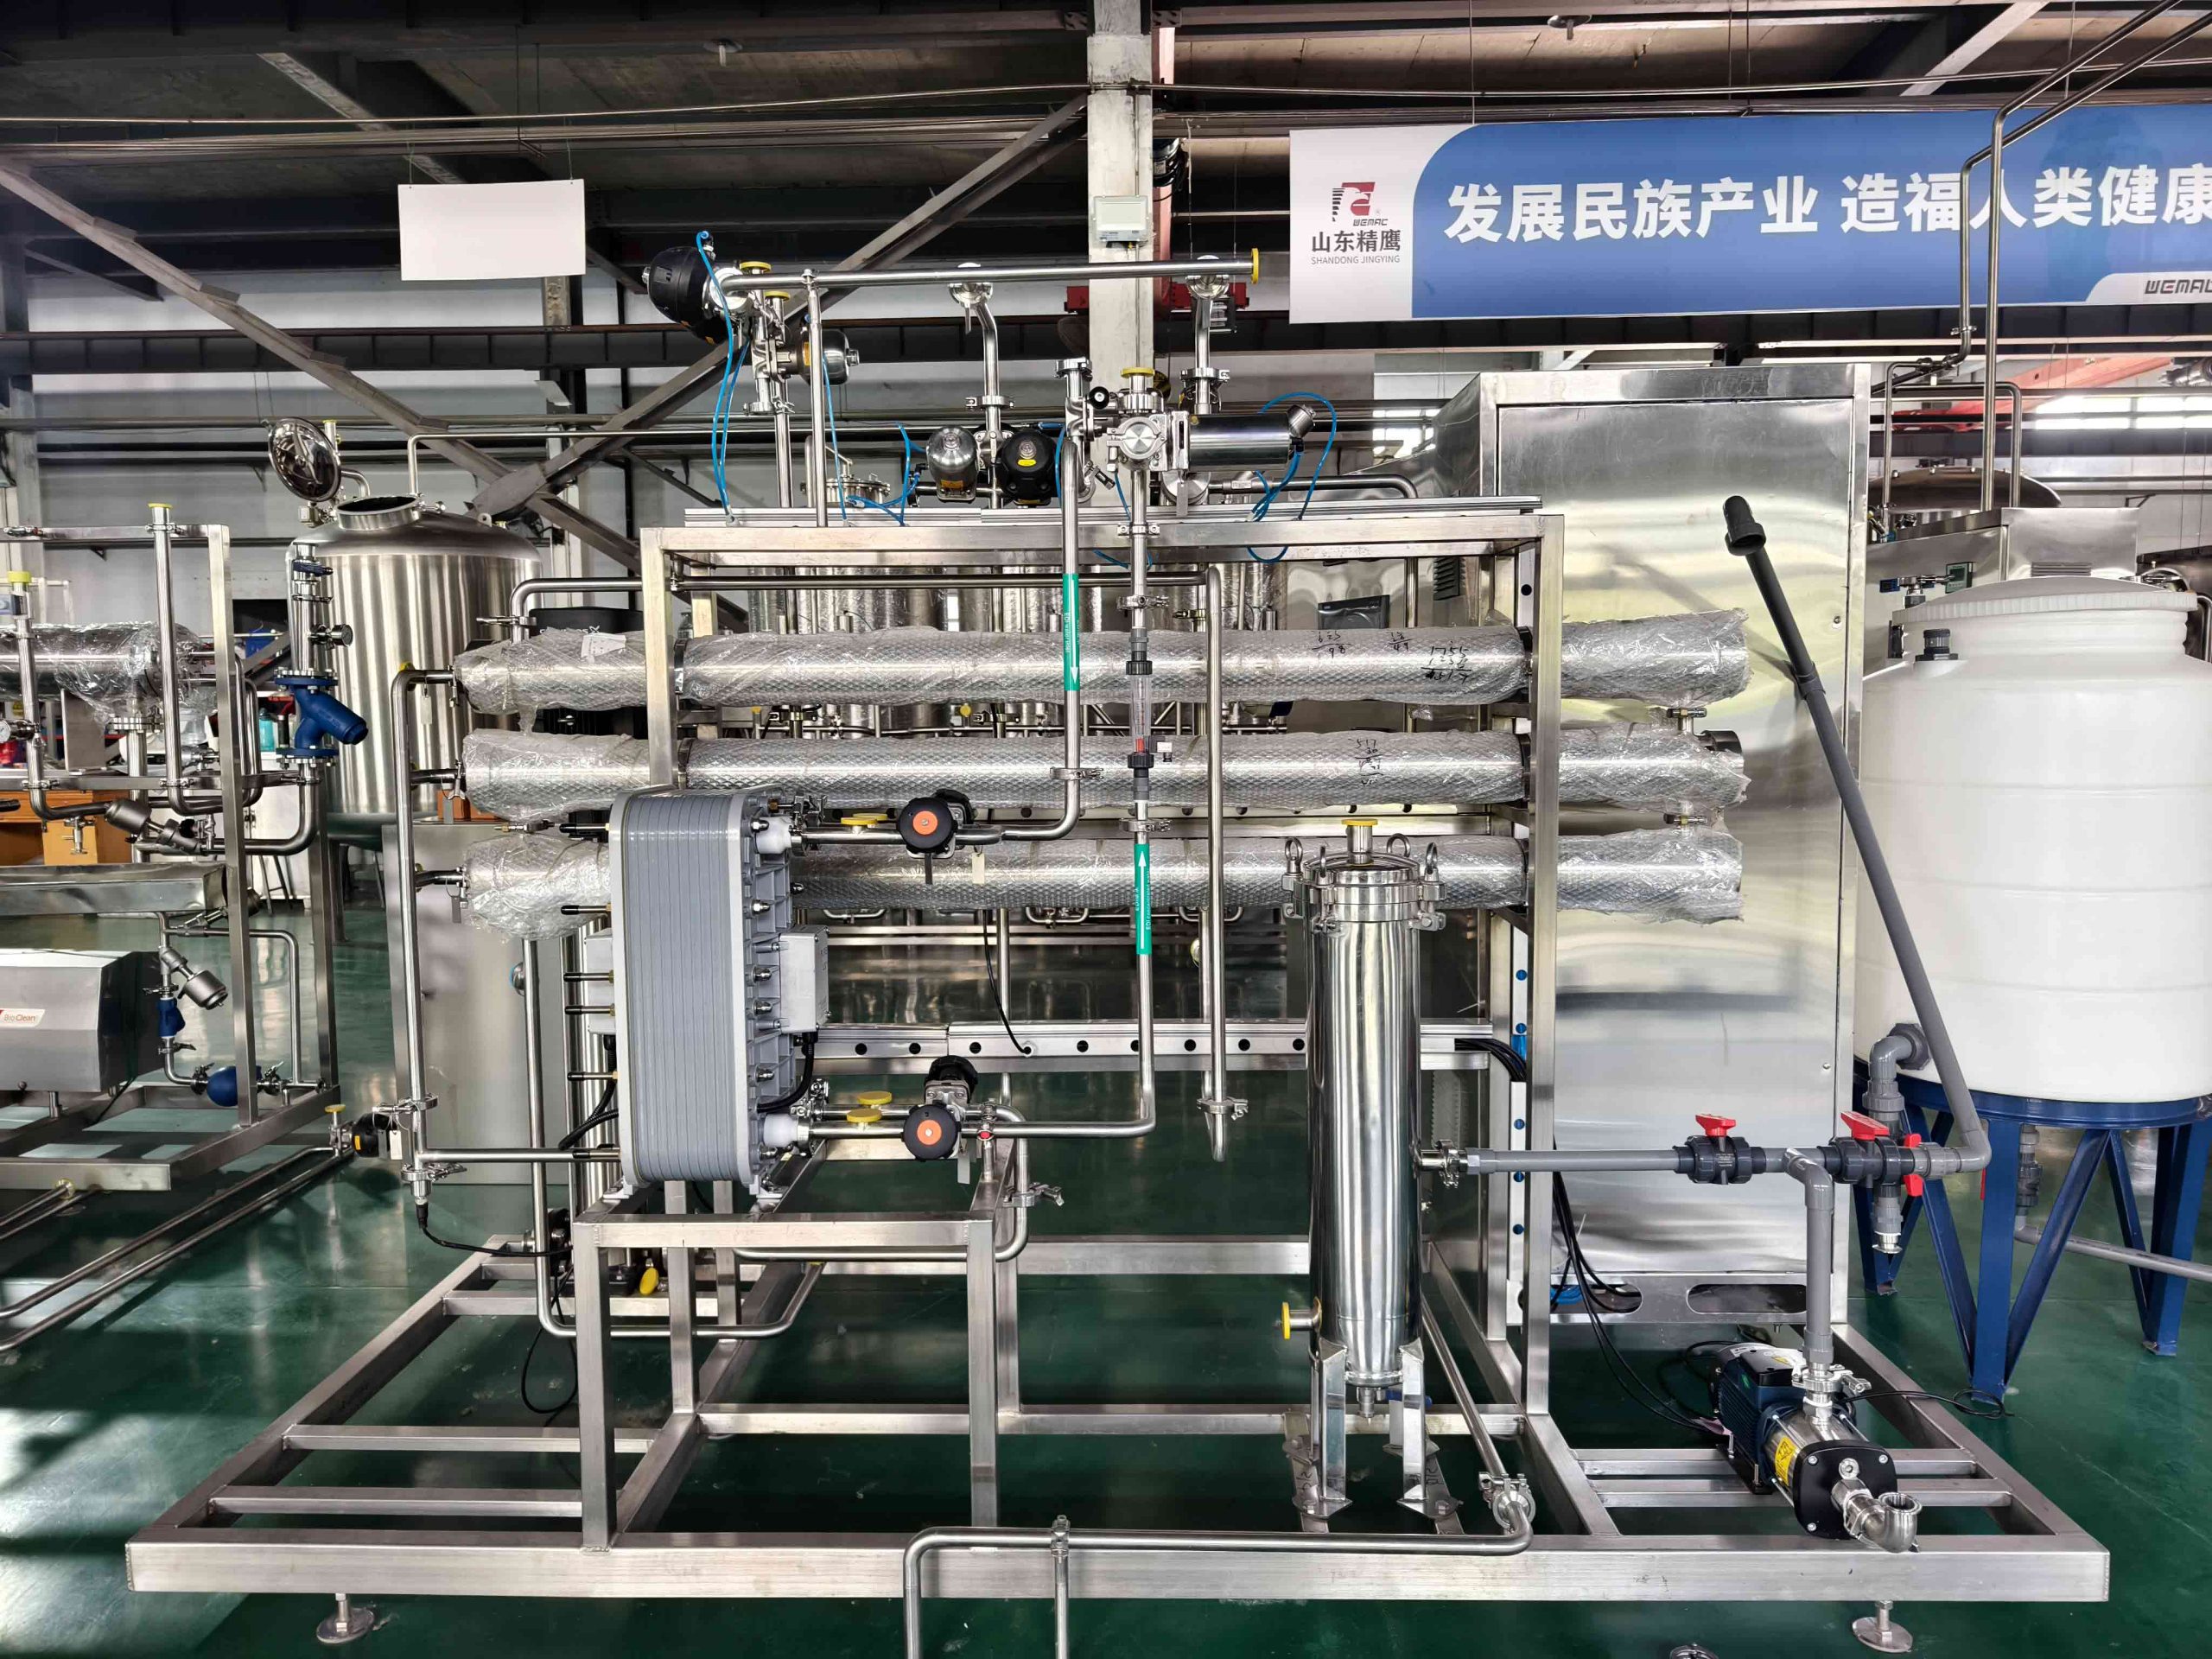
A typical purified water preparation system uses multiple purification stages, including pretreatment, reverse osmosis, polishing technologies, and storage and distribution.
Common technologies for producing purified water include:
- Reverse osmosis (RO)
- Electrodeionization (EDI)
- Ultrafiltration
- Ion exchange systems
The final water quality must comply with the requirements of applicable pharmacopoeias, such as USP, EP, or ChP.
Water for Injection (WFI)
Water for Injection is the highest-grade pharmaceutical water used mainly for sterile manufacturing processes.
WFI is required for applications such as:
- Injectable drug production
- Final rinsing of sterile equipment
- Sterile API manufacturing
- Ophthalmic product production
Compared with purified water, WFI requires much stricter control of microbial contamination and endotoxin levels. The production and distribution system must be carefully designed to prevent microbial growth and maintain stable water quality.
Core Technologies of a Pharmaceutical Water Preparation System
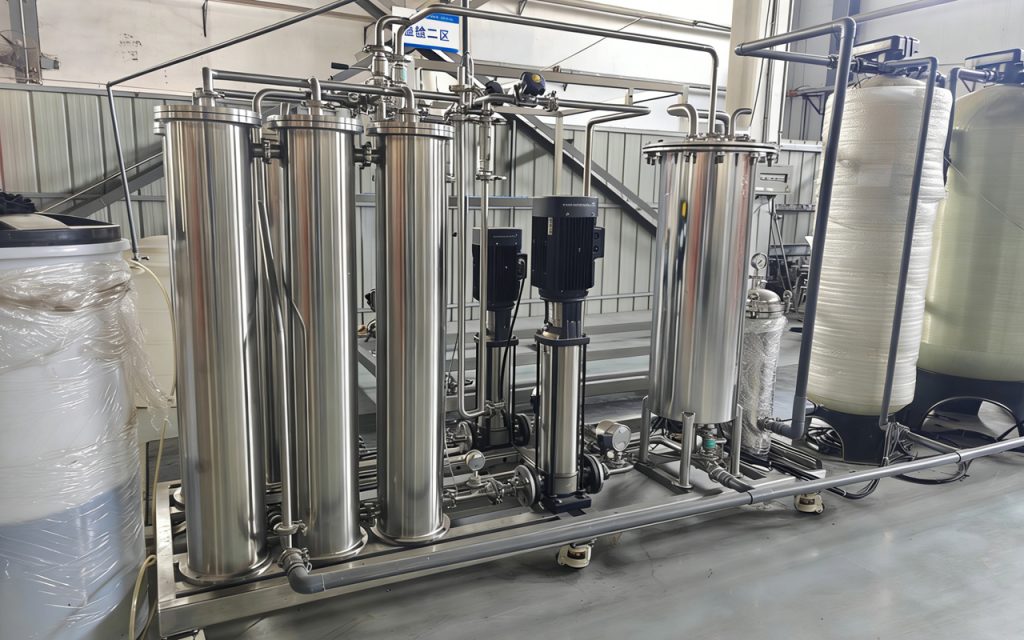
A complete pharmaceutical water preparation system usually includes three major sections:
- Pretreatment system
- Purification system
- Storage and distribution system
Each section plays an important role in maintaining stable water quality.
Pretreatment System
Pretreatment protects the main purification equipment by removing impurities from the feed water.
Typical pretreatment processes include:
- Multimedia filtration
- Activated carbon filtration
- Water softening
- Cartridge filtration
These processes help remove suspended particles, chlorine, hardness, and organic substances that may damage RO membranes or affect system performance.
The design of pretreatment should consider local water conditions, seasonal changes, and production requirements.
Reverse Osmosis and EDI Technology
Reverse osmosis is one of the most widely used purification technologies in pharmaceutical water production.
RO systems use high pressure to force water through a semi-permeable membrane. The membrane removes dissolved salts, organic compounds, microorganisms, and other impurities.
For many pharmaceutical applications, RO is the main purification step in a purified water preparation system.
For higher purity requirements, RO is often combined with Electrodeionization (EDI).
EDI uses ion exchange technology and an electric field to continuously remove ions without chemical regeneration. Compared with traditional ion exchange systems, EDI provides:
- Stable water quality
- Lower chemical consumption
- Easier operation
- Better environmental performance
RO+EDI has become a common configuration for modern pharmaceutical purified water systems.
WFI Preparation System Technologies
A WFI preparation system requires more advanced purification technology because it must achieve extremely high microbial and endotoxin control.
The two main technical approaches include distillation and membrane-based systems.
Multi-Effect Distillation System
Multi-effect distillation (MED) is a traditional technology for WFI production.
The system uses repeated evaporation and condensation processes to separate purified water from contaminants. Because endotoxins and microorganisms cannot easily transfer with pure steam condensation, distillation provides excellent purification performance.
Advantages of multi-effect distillation include:
- Long compliance history
- High reliability
- Excellent endotoxin removal capability
- Suitable for strict sterile production environments
For many pharmaceutical companies, MED remains a preferred solution, especially when regulatory acceptance and long-term reliability are key considerations.
Membrane-Based WFI Production
In recent years, membrane-based WFI production technologies have become more widely accepted in some markets.
A membrane-based WFI system may combine:
- Reverse osmosis
- Ultrafiltration
- Advanced monitoring systems
Compared with distillation systems, membrane technologies usually operate at lower temperatures and can reduce energy consumption.
However, membrane-based WFI systems require strong risk control, including:
- Effective microbial control
- Biofilm prevention
- Online monitoring
- Regular validation testing
The final technology selection should consider regulatory requirements, production risks, and the company’s validation capability.
Storage and Distribution System Design
Producing high-quality pharmaceutical water is only part of the solution. Proper storage and distribution are equally important.
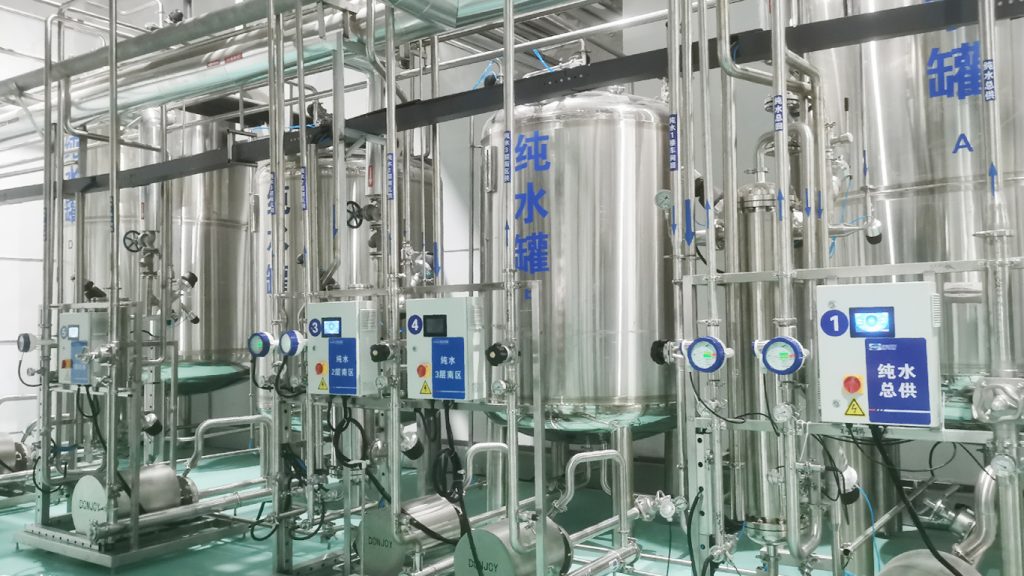
A pharmaceutical water distribution system normally includes:
- Stainless steel storage tanks
- Circulation pumps
- Sanitary piping loops
- Online monitoring instruments
The system design should minimize contamination risks by avoiding:
- Dead legs
- Low-flow areas
- Poor drainage structures
For WFI systems, hot water circulation is commonly used to control microbial growth. High-quality 316L stainless steel piping with proper surface treatment is often selected for pharmaceutical applications.
How to Select the Right Pharmaceutical Water System
Choosing the correct pharmaceutical water preparation system requires consideration of several factors.
Product Requirements
The first step is identifying the required water grade.
For example:
- Non-sterile oral products usually require purified water
- Injectable products generally require WFI
- Biological products may require higher control levels depending on the process
Feed Water Quality
Raw water conditions directly affect system design.
Important factors include:
- Conductivity
- Hardness
- Chlorine content
- Organic contamination
- Seasonal variation
A suitable pretreatment system can improve equipment stability and reduce maintenance costs.
Production Capacity and Operating Cost
The system should match actual production demand.
Oversized systems may increase investment and energy costs, while undersized systems may affect production efficiency.
A professional supplier should evaluate:
- Daily water consumption
- Peak demand
- Storage capacity
- Distribution loop design
Validation and Monitoring of Pharmaceutical Water Systems
A pharmaceutical water system must be validated before commercial operation.
Typical validation stages include:
Installation Qualification (IQ)
IQ confirms that equipment installation meets approved design specifications.
Operational Qualification (OQ)
OQ verifies that the system operates correctly under defined operating conditions.
Performance Qualification (PQ)
PQ confirms that the system can continuously produce pharmaceutical water that meets quality requirements.
Routine monitoring usually includes:
- Conductivity testing
- Total Organic Carbon (TOC) monitoring
- Microbial testing
- Endotoxin testing for WFI systems
Trend analysis is also important. Continuous monitoring helps identify potential problems before water quality falls outside acceptable limits.

Complete Pharmaceutical Water Solutions from SKE&EAGLE
SKE&EAGLE specializes in the design and manufacturing of pharmaceutical water preparation systems for pharmaceutical, biotechnology, and healthcare industries.
We provide complete solutions including:
- Pretreatment systems
- Purified water preparation systems
- WFI preparation systems
- Storage tanks
- Distribution loops
- Validation support
With professional engineering experience, GMP-focused design, and customized solutions, SKE&EAGLE helps customers build reliable pharmaceutical water systems that meet international quality requirements.
FAQ
1. What is the difference between purified water and WFI?
Purified water and WFI have different quality requirements. WFI requires stricter control of endotoxins and microbial contamination and is mainly used for sterile pharmaceutical applications such as injections.
2. Can RO technology be used for WFI production?
Yes, membrane-based technologies such as RO combined with ultrafiltration can be used for WFI production in some regulatory markets. However, companies must establish strong microbial control strategies and complete validation procedures.
3. What technologies are commonly used in purified water systems?
Common technologies include reverse osmosis, EDI, ultrafiltration, and other polishing processes. RO+EDI is one of the most widely used configurations for modern purified water systems.
4. How often should pharmaceutical water systems be sanitized?
Sanitization frequency depends on system design, operating conditions, and validation results. Purified water systems may use hot water or chemical sanitization, while WFI systems often use high-temperature circulation control.
5. How do companies choose between a distillation WFI system and a membrane WFI system?
The choice depends on regulatory requirements, energy considerations, production needs, and validation strategy. Pharmaceutical companies should evaluate both technical performance and long-term compliance requirements.
Contact SKE & Eagle for Advanced Solutions
For customized system engineering solutions or integration of high-performance water treatment technologies, please contact SKE & Eagle. Our professional team collaborates closely with industrial partners to design, implement, and maintain solutions tailored to your operational needs.
Official Website: https://www.ske-eagle.com/
Contact Email: info@ske-eagle.com
Follow us on Facebook for the latest industry insights: SKE & Eagle Facebook
Business Inquiries: Visit our official website and submit the contact form at the bottom.